Molds built in‑house, sized to your run.
After the prototype is approved we design the mold in SolidWorks, run a mold-flow analysis, lay out the cooling water and ejector pins, then cut it on our own computer-controlled mills and EDM machines. Single cavity, multi-cavity, or a family mold that makes all the parts of an assembly in one shot.
Pick the steel by how many parts you need.
The mold material is the main cost lever. We'll recommend one based on your volume, finish and resin.
| Mold material | Good for | Notes |
|---|---|---|
| Aluminum | Up to 100,000 to 300,000 parts | Lowest cost and fastest to cut. The usual choice for new products and moderate runs. |
| P-20 steel | Up to about one million parts | Pre-hardened tool steel. The workhorse for most production molds. |
| H-13 steel, hardened | More than one million parts | For long runs and abrasive or glass-filled resins. |
| 420 stainless | Any volume | Where a highly polished, mirror finish is wanted on the part. |
| MUD inserts | Smaller parts | Master Unit Die inserts that fit our standard bases, which cuts the cost of a small mold. |
The mold shop.
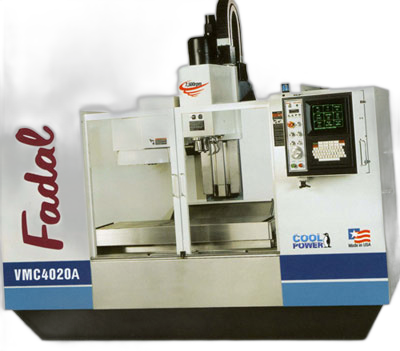
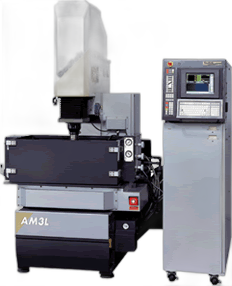
Because the mold is designed and cut in the same building where it will run, the people who machine it are the same people who will set it in the press. Problems get found at the bench, not on the floor.